A new collet can show runout even before it completes its first machining operation. The problem does not always mean the collet is defective. Incorrect seating, contamination, tool shank errors, or spindle conditions can affect the final reading.
New collet runout becomes especially confusing when an operator replaces an old collet but sees little improvement in machining accuracy. In some cases, the reading becomes worse after replacement.
The correct approach is to inspect the complete clamping assembly before blaming the new component. For example, precision ER collets depend on proper seating, compatible holders, and correct assembly to deliver consistent tool positioning.
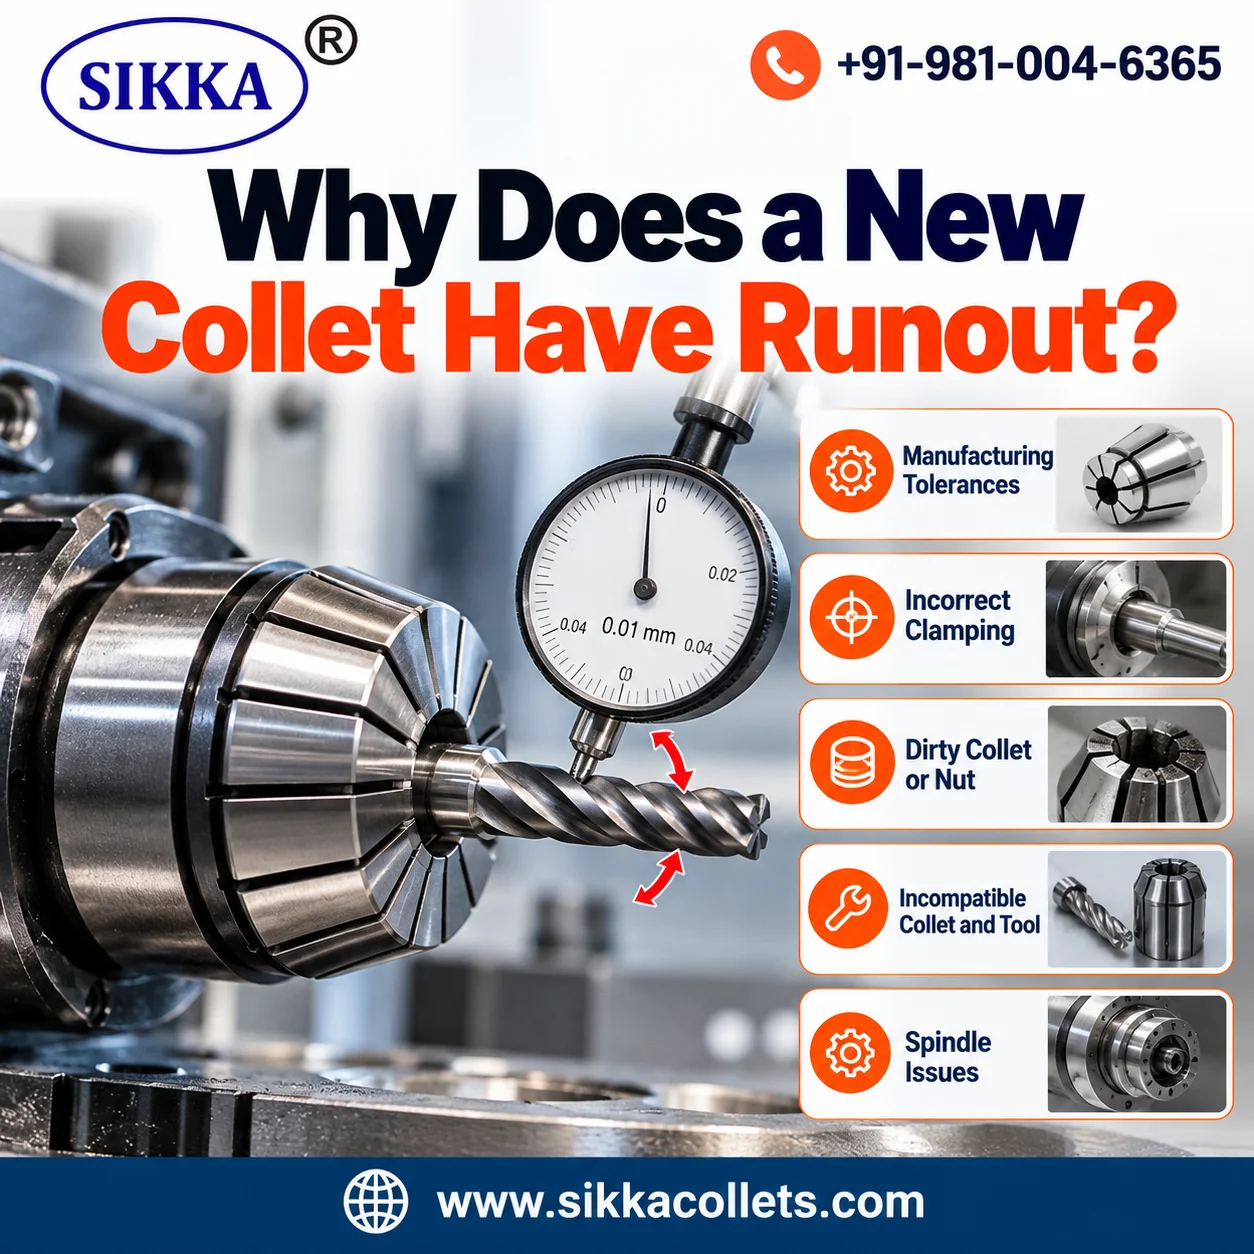
Is the Runout Coming From the Collet or the Machine?
The first step is to identify where the error begins. A dial indicator measures the combined movement of the components involved in the test. It does not automatically identify the defective part.
A reading taken on a tool shank may include errors from the collet, holder, spindle, and tool itself. This makes component isolation important.
Consider two situations. In the first, a new collet produces excessive runout in one holder but performs correctly in another compatible holder. This suggests the original holder or its interface needs inspection.
In the second, several compatible collets produce similar readings in the same spindle. The operator should investigate the spindle and holder before purchasing another collet.
These comparisons are diagnostic clues. They do not replace proper measurement or manufacturer specifications.
What Changes When You Install a New Collet?
Replacing a collet changes more than the gripping component. The operator also releases the tool, opens the clamping assembly, and creates new contact between several precision surfaces.
Small changes during this process can affect concentricity.
Contact Surfaces May Not Seat Correctly
A small chip or hardened coolant deposit can prevent uniform contact. The collet may then sit at a slight angle inside the holder.
Even a correctly manufactured collet cannot compensate for an obstructed seating surface.
Clamping Conditions May Change
Different tightening methods can produce inconsistent seating. Incorrect nut assembly may also affect how the collet grips the tool.
Operators should follow the recommended assembly sequence and tightening torque for their specific system.
The Replacement May Not Match the Application
Collets are available in different systems, dimensions, and gripping ranges. A similar appearance does not guarantee compatibility.
Check the collet designation, tool shank diameter, and holder specification before installation.
Seven Checks to Find the Source of New Collet Runout
New collet runout should be investigated through controlled checks. Avoid changing several components at once. Otherwise, identifying the original problem becomes difficult.
1. Inspect the Collet Bore and External Taper
Start with the new collet itself. Examine its gripping bore and external contact surfaces under suitable lighting.
Look for burrs, scratches, corrosion, or visible manufacturing damage. Check for contamination inside the bore.
Do not attempt to correct a precision surface by uncontrolled grinding or polishing. Such work can change the component’s geometry.
2. Clean the Holder and Spindle Interfaces
Remove the collet and inspect the seating surfaces. Metal chips, dried coolant, and dirt can prevent proper contact.
Use cleaning methods recommended for the equipment. Protect precision surfaces from scratches.
Reassemble the system after cleaning. Then repeat the measurement under the same conditions.
3. Confirm the Tool Shank Diameter
A collet must grip a compatible shank within its specified range. An incorrect diameter can affect gripping contact and tool positioning.
Measure the shank with a suitable micrometer. Check for wear, damage, and dimensional variation.
Compare the measurement with the collet manufacturer’s stated gripping range.
4. Examine the Collet Nut and Assembly
A damaged nut or incorrect assembly can prevent proper seating. Some ER systems require the collet to engage with the nut’s retaining ring before the assembly enters the holder.
Check the applicable manufacturer’s instructions before tightening.
Inspect the nut for thread damage and worn contact surfaces. Replace damaged components rather than forcing the assembly together.
5. Check the Cutting Tool or Test Bar
A bent tool can produce an excessive indicator reading even when the collet is correctly seated.
Use a suitable precision test bar when possible. Inspect its surface and confirm that it meets the measurement requirements.
Avoid relying on an unknown or visibly damaged cutting tool for accuracy testing.
6. Measure the Holder and Spindle Separately
When practical, check accessible spindle and holder reference surfaces using the equipment manufacturer’s measurement procedure.
Compare these readings with the complete tool assembly.
If the underlying interface already shows excessive runout, replacing the collet alone may not solve the problem.
7. Repeat the Test After Reclamping
Remove and reinstall the test bar using the same procedure. Repeat the measurement several times.
Changes between readings may indicate inconsistent seating, contamination, or clamping conditions.
Stable readings help establish a reliable baseline for further inspection.
How to Measure Runout Without Misdiagnosing the Collet?
Accurate measurement requires a consistent setup. New collet runout cannot be assessed reliably if the measurement method changes between tests.
Prepare the Measurement Setup
Use a suitable dial test indicator, rigid indicator stand, and precision test bar. Confirm that the machine is secured against unintended startup.
Clean the contact surfaces and install the test bar according to the manufacturer’s instructions.
Record the Total Indicated Runout
Position the indicator against the test bar at a defined distance from the collet face.
Rotate the spindle slowly by hand only when the machine manufacturer’s safety procedure permits it. Observe the highest and lowest indicator readings.
The difference between these readings is the total indicated runout, commonly called TIR.
TIR = Maximum indicator reading – Minimum indicator reading
Record the measurement position and test conditions. Without these details, comparing readings can be misleading.
Measure at Two Positions
Take one reading close to the collet face and another farther along the test bar.
If runout increases with distance, angular misalignment may be contributing to the error. However, test bar straightness and measurement setup must also be considered.
Do not treat a single TIR value as proof of a defective collet.
Read the Symptoms Before Replacing the Collet
Different measurement patterns can help narrow the investigation. The following table provides possible explanations and appropriate next checks.
| Observed Symptom | Possible Cause | Next Check |
| High runout immediately after installation | Contamination or incorrect seating | Inspect and clean contact surfaces |
| Runout changes after reclamping | Inconsistent assembly or gripping | Repeat the approved clamping procedure |
| Several collets show similar runout | Holder or spindle condition | Measure the relevant reference surfaces |
| Runout increases farther from the collet | Angular error or test bar condition | Check alignment and bar straightness |
| One tool shows more runout than others | Shank damage or dimensional mismatch | Inspect and measure the tool shank |
These observations guide troubleshooting. Confirm the actual cause through repeatable measurements.
When Should You Reject or Replace a New Collet?
Not every visible runout reading justifies replacement. First, confirm that the collet is compatible with the holder and tool.
Inspect the assembly and repeat the test using verified measuring equipment.
Replacement may be appropriate when the collet has visible damage, incorrect dimensions, or repeatable runout beyond its specified acceptance limits under the manufacturer’s test conditions.
There is no single universal TIR limit suitable for every collet system. Permissible values depend on the component design, accuracy grade, measurement distance, and application.
Compare the result with the relevant product specification rather than an unsupported general tolerance.
How Collet Type and Holder Compatibility Affect Runout?
Collet selection influences how the tool or workpiece is positioned and clamped. Different systems use different gripping mechanisms and contact geometries.
For example, ER systems are commonly used for tool holding. Other collet designs support specific turning, workholding, or production requirements.
The condition and compatibility of collet holders are important because the holder provides the seating interface for the collet assembly.
Operators should confirm the complete system designation before selecting replacement parts. Matching the nominal tool diameter alone is not sufficient.
For CNC applications, inspect the relevant CNC collet chucks and their specified interfaces when investigating repeated alignment problems.
Frequently Asked Questions
Can a New Collet Have Manufacturing Runout?
Yes. Manufacturing errors can affect concentricity. However, an excessive assembly reading does not prove a manufacturing defect. Verify the collet under appropriate inspection conditions.
Can a Dirty Spindle Cause Runout With a New Collet?
Yes. Contamination on precision contact surfaces can prevent correct seating. Cleaning and rechecking the assembly may help identify the issue.
Why Does Runout Change After Reclamping?
Changes may result from inconsistent seating, debris, incorrect assembly, or variations in tool positioning. Repeat the test with controlled conditions.
Should a New Collet Always Show Zero Runout?
No. Real components have manufacturing tolerances. The important question is whether the measured runout meets the applicable specification under defined test conditions. When new collet runout persists, compare repeatable measurements across the collet, tool, holder, and spindle. This approach helps identify the responsible component before unnecessary replacement.