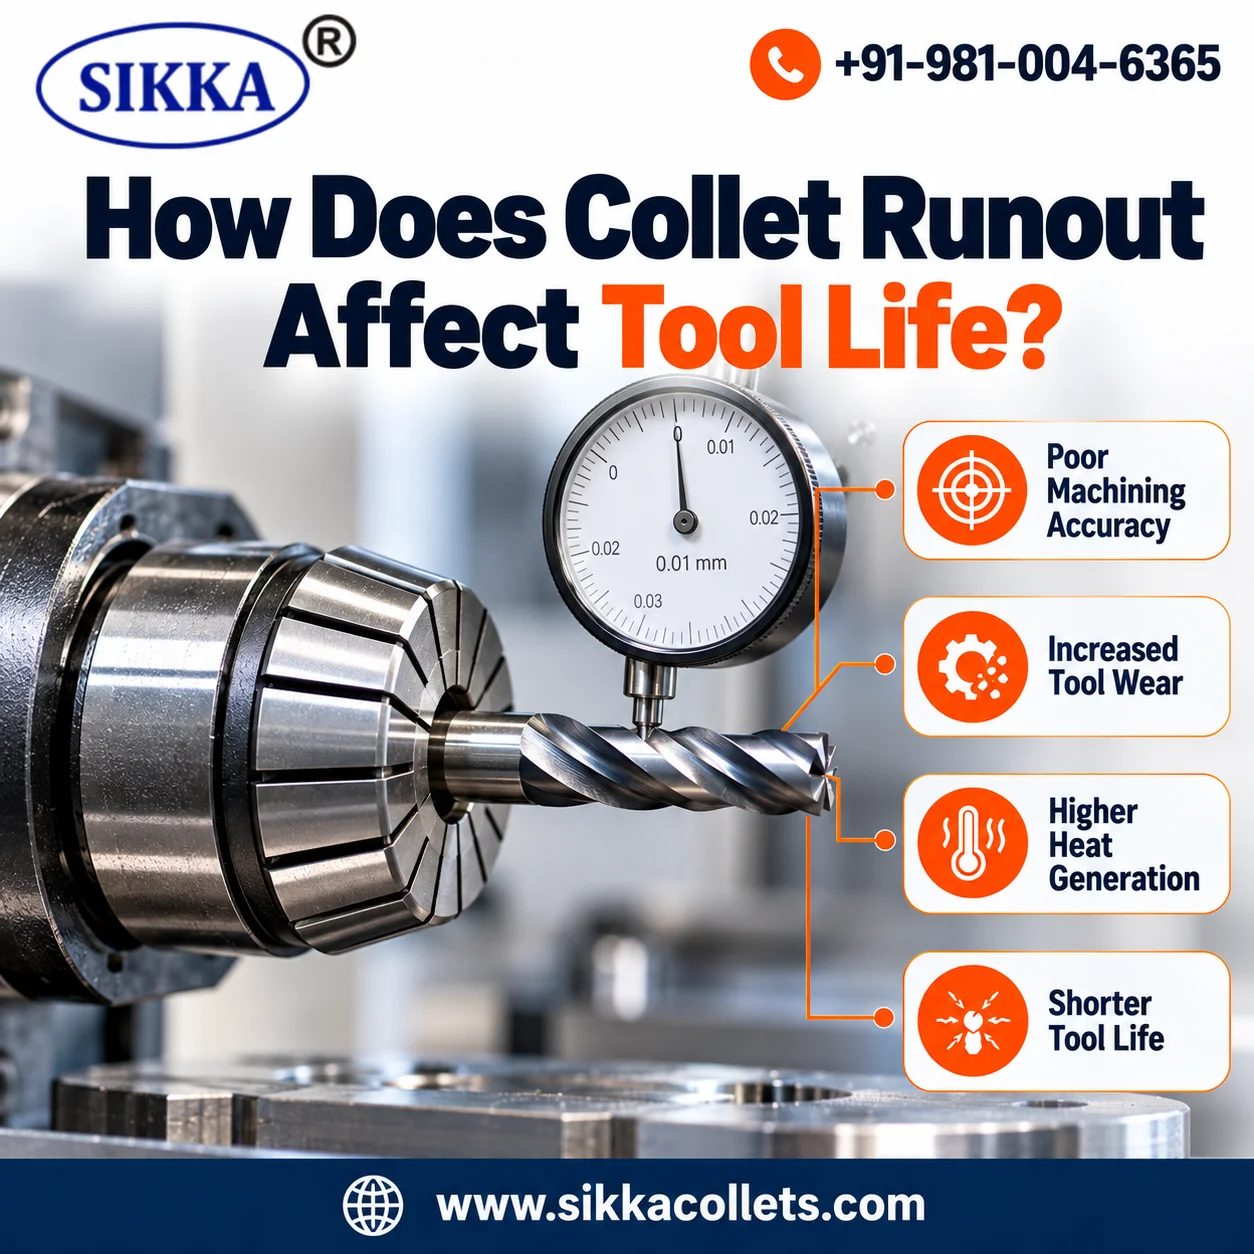
Collet runout can reduce cutting tool life by creating uneven cutting forces during CNC machining. One cutting edge may remove more material than the others. This can cause faster wear, edge chipping, vibration, and early tool failure. Excessive runout can also affect surface finish and dimensional accuracy.
The problem may come from a worn collet, dirty contact surfaces, incorrect clamping, or a damaged toolholder. Spindle issues and bent tool shanks can also contribute. Identifying the actual cause helps prevent repeated tool changes and unnecessary production costs.
What Is Collet Runout in CNC Machining?
Collet runout is the variation in a tool’s radial position as it rotates in a collet holding system. Ideally, the tool should rotate around its intended axis. Excessive runout means the tool does not rotate accurately around that axis.
In CNC machining, the collet grips the tool shank inside a holder. Correct fit and seating are essential for accurate rotation. Chips, wear, or incorrect assembly can affect contact between these components.
Runout is commonly checked using Total Indicated Runout (TIR). A dial indicator records the highest and lowest readings during rotation. The difference between them is the TIR. For example, readings of 0.012 mm and 0.004 mm produce a TIR of 0.008 mm.
How Does Collet Runout Reduce Tool Life?
1. Uneven Cutting Forces and Faster Tool Wear
Excessive collet runout changes how cutting edges engage with the workpiece. One flute may carry a greater share of the cutting load. Other flutes may remove less material. This uneven loading can cause faster wear on individual cutting edges.
The problem can be important when machining hard materials or using small-diameter cutters. A heavily loaded edge may lose its sharpness sooner. It may also develop local damage that affects cutting performance.
2. Cutting Edge Chipping and Tool Breakage
Uneven cutting forces can increase stress on individual cutting edges. This may raise the risk of chipping, especially when machining hard materials or using brittle carbide tools. Interrupted cuts and aggressive cutting conditions can make the problem worse.
Inspect the cutting edges when a tool fails earlier than expected. Uneven wear across the flutes can indicate a possible runout problem. However, check tool geometry, cutting parameters, and workpiece rigidity before blaming the collet.
3. Vibration, Chatter, and Heat
Runout can disturb the balance of cutting forces during machining. This may increase vibration and chatter. These effects depend on the tool, machine, workpiece, and cutting conditions.
Chatter can leave visible marks on the finished surface. It can also increase stress on the cutting edges. Extra friction may contribute to heat generation and faster wear.
Check tool stick-out, clamping, and cutting parameters when vibration appears. Inspect the holder and collet for damage. Replacing the collet alone may not solve the problem if the spindle is responsible.
4. Poor Surface Finish and Dimensional Accuracy
Runout can make cutting edges remove different amounts of material. This may create uneven surface marks and affect final dimensions. The impact depends on the runout level and the accuracy required for the component.
These problems can lead to additional inspection, rework, or rejected parts. A consistent toolholding setup helps maintain machining quality and reduces avoidable production interruptions.
Common Causes of Excessive Collet Runout
Collet runout can develop even when the collet looks undamaged. Small problems with fit, cleanliness, or assembly can affect tool rotation.
- Dirty contact surfaces: Chips and dried coolant can prevent the collet from seating correctly.
- Worn collet: Repeated use or damage can affect gripping accuracy.
- Incorrect collet size: The collet must match the tool shank and specified clamping range.
- Damaged holder or nut: Worn tapers, damaged threads, or incorrect assembly can affect alignment.
- Bent tool shank: A damaged tool may show runout even with a suitable collet.
- Spindle issues: Spindle condition or bearing problems may contribute to runout across multiple setups.
For milling operations, compatible milling collets should match the toolholding system and application. Correct fit and assembly are essential for reliable clamping.
How to Measure Collet Runout?
A dial indicator can help identify excessive runout. Use a suitable measuring setup and follow the machine manufacturer’s safety instructions.
- Clean the components: Remove chips and residue from the collet, holder, tool shank, and contact surfaces.
- Inspect the assembly: Check the collet, nut, holder, and tool for visible wear or damage.
- Fit the tool correctly: Assemble the collet and nut according to the manufacturer’s instructions.
- Position the indicator: Place it against a suitable cylindrical surface on the tool shank or a precision test bar.
- Record the readings: With the spindle stopped, rotate the assembly by hand if the setup permits. Record the maximum and minimum readings.
- Calculate TIR: Subtract the minimum reading from the maximum reading. Compare the result with the tolerance required for the application.
Compare readings at different positions along the tool or test bar. This can help reveal angular misalignment or tool geometry issues. If runout remains high after cleaning and correct assembly, inspect the holder and spindle using an appropriate procedure.
How to Reduce Collet Runout and Extend Tool Life?
Clean and Inspect Before Assembly
Remove chips, dust, and coolant residue from contact surfaces. Inspect the collet slots, holder taper, and nut for damage. Replace components that do not meet the manufacturer’s requirements. Avoid using damaged collets simply because they still grip the tool.
Use the Correct Collet and Clamping Method
Choose a collet that matches the tool shank diameter and specified clamping range. Do not force an incorrectly sized collet onto a tool. Follow the recommended assembly and tightening procedure. Use the correct spanner and avoid excessive tightening.
Keep tool stick-out as short as the machining operation allows. A shorter overhang can improve rigidity, although it does not correct runout caused by a damaged component.
Check Runout After Tool Changes
Measure runout when installing a new tool, replacing a collet, or investigating unusual wear. Set an inspection frequency based on the machining process and accuracy requirements. Record readings when repeatability is important.
If runout remains high, check the tool, collet, holder, and spindle systematically. Compatible CNC collet chucks can support accurate toolholding when correctly matched with the machine and collet system. However, no holder can compensate for every source of runout.
How to Choose Collets for Better Tool Life?
Collet selection should match the machine, toolholder, tool shank, and machining operation. Check the manufacturer’s accuracy specifications and confirm that they apply to the intended setup. Consider clamping range, material quality, operating speed, and holder compatibility.
Do not select a collet based on size or appearance alone. A precision collet may help reduce runout when the rest of the toolholding system is in good condition. Actual tool life also depends on tool geometry, workpiece material, cutting parameters, and machine stability.
For suitable turning applications, lathe collets may be an option when their specifications match the machine and workholding requirements.
Frequently Asked Questions
What Is an Acceptable Collet Runout for CNC Machining?
There is no universal limit for every application. The acceptable value depends on tool diameter, machining operation, holder system, and accuracy requirements. Follow the manufacturer’s specifications.
Can Collet Runout Cause Tool Breakage?
Yes. Excessive runout can increase uneven cutting forces and stress on individual cutting edges. This may raise the risk of chipping or breakage. Incorrect cutting parameters and poor clamping can also cause tool failure.
How Often Should CNC Collets Be Inspected?
Inspect collets during routine maintenance and whenever vibration, unusual wear, or surface finish problems appear. High-precision operations may require more frequent checks.
Can Precision Collets Improve Tool Life?
A suitable precision collet can help reduce runout when the holder, tool, and spindle are in good condition. More consistent cutting-edge loading may support longer tool life. Results depend on the complete machining setup.
Conclusion
Collet runout can shorten tool life through uneven cutting forces, edge wear, vibration, and dimensional variation. Accurate measurement helps identify problems before they lead to repeated tool failures or quality issues.
Keep contact surfaces clean, use compatible components, and inspect the complete toolholding system when readings exceed the required limits. These practices help maintain consistent machining performance and support more reliable tool replacement decisions.